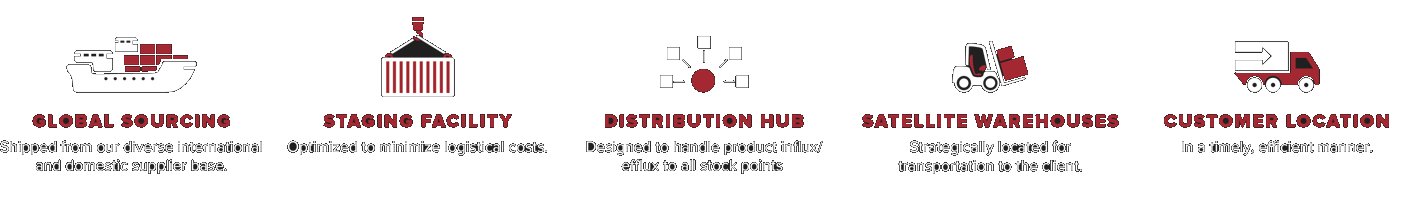
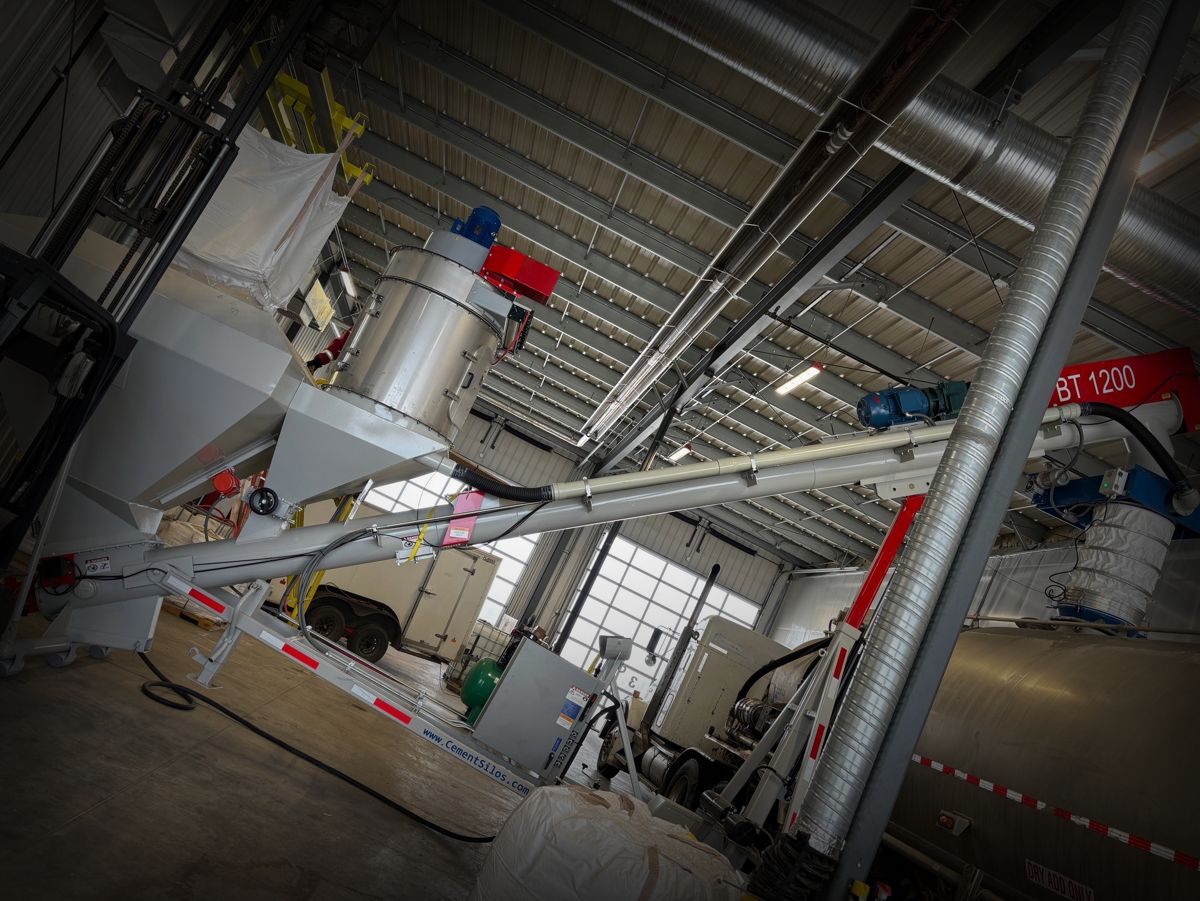
Logistical authority is anchored by our ability to process and move high-volume completion chemicals at scale. Our indoor, temperature-controlled terminal in Grande Prairie serves as a critical hub for dry friction reducer and dry guar powder logistics, built for speed, safety, and scale.
Our facility completes 17-tonne truck loads in under one hour, ensuring minimal turnaround times for bulk logistics.
The terminal is capable of processing up to 70 metric tons per day to meet the demands of high-intensity programs.
A dual-entry indoor design ensures seamless bulk truck movement while protecting product integrity throughout all weather conditions.
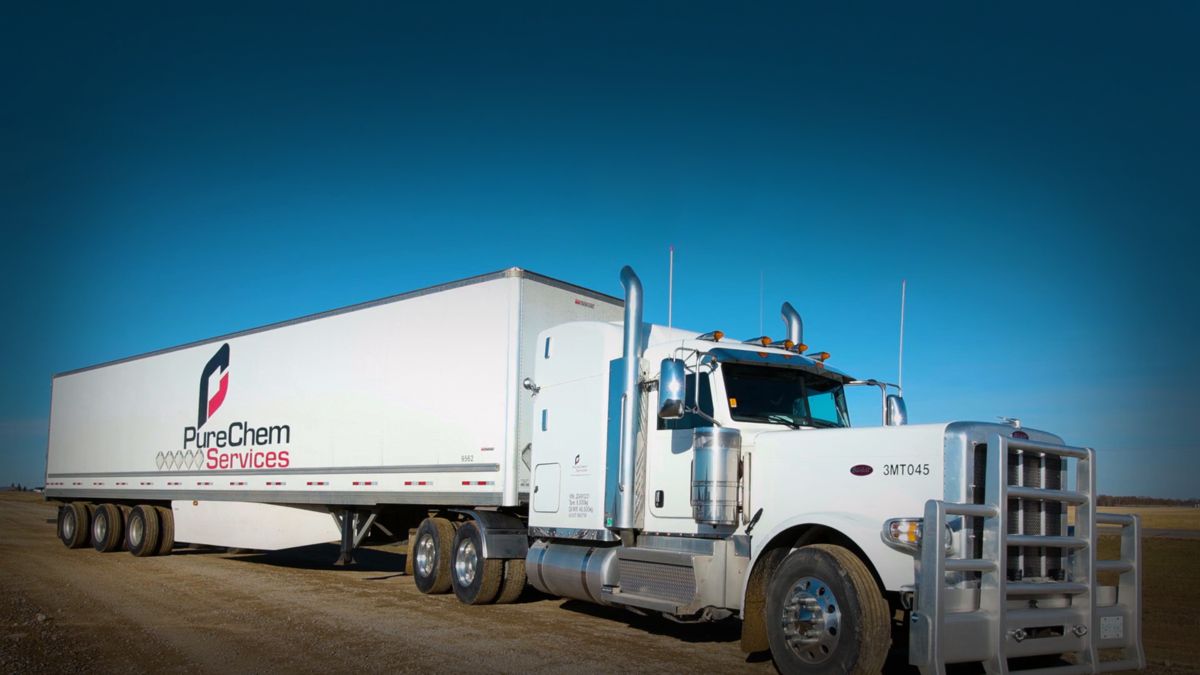
The last mile of delivery is where chemical performance is often compromised by temperature fluctuations. We operate a specialized, private fleet to ensure every molecule arrives at the wellhead exactly as it was formulated.
Specifically designed for heated tote transfer, these units maintain a consistent internal environment to preserve the integrity of friction reducers and our product line.
High-capacity, insulated units designed for bulk-to-bulk transfer during large-volume operations.
Supported by ample heated storage and blending capacity to guarantee chemical reliability right where you need it.
Strategically positioned bases in Calgary, Nisku, Carlyle, and Grande Prairie ensuring 24/7 delivery support and optimized mobilization times.
In the Canadian winter, chemical stratification and freezing are primary drivers of operational delays and issues. Our specialized storage tanks ensure that every load remains protected in its ideal state for pumpability.
Specialized 90 m³ storage units featuring high-output heating and agitation systems to ensure quality control even in the harsh winter climates of the WCSB.
Mechanical agitation ensures rigorous quality control and assurance, delivering a consistent product blend from the first load to the last.
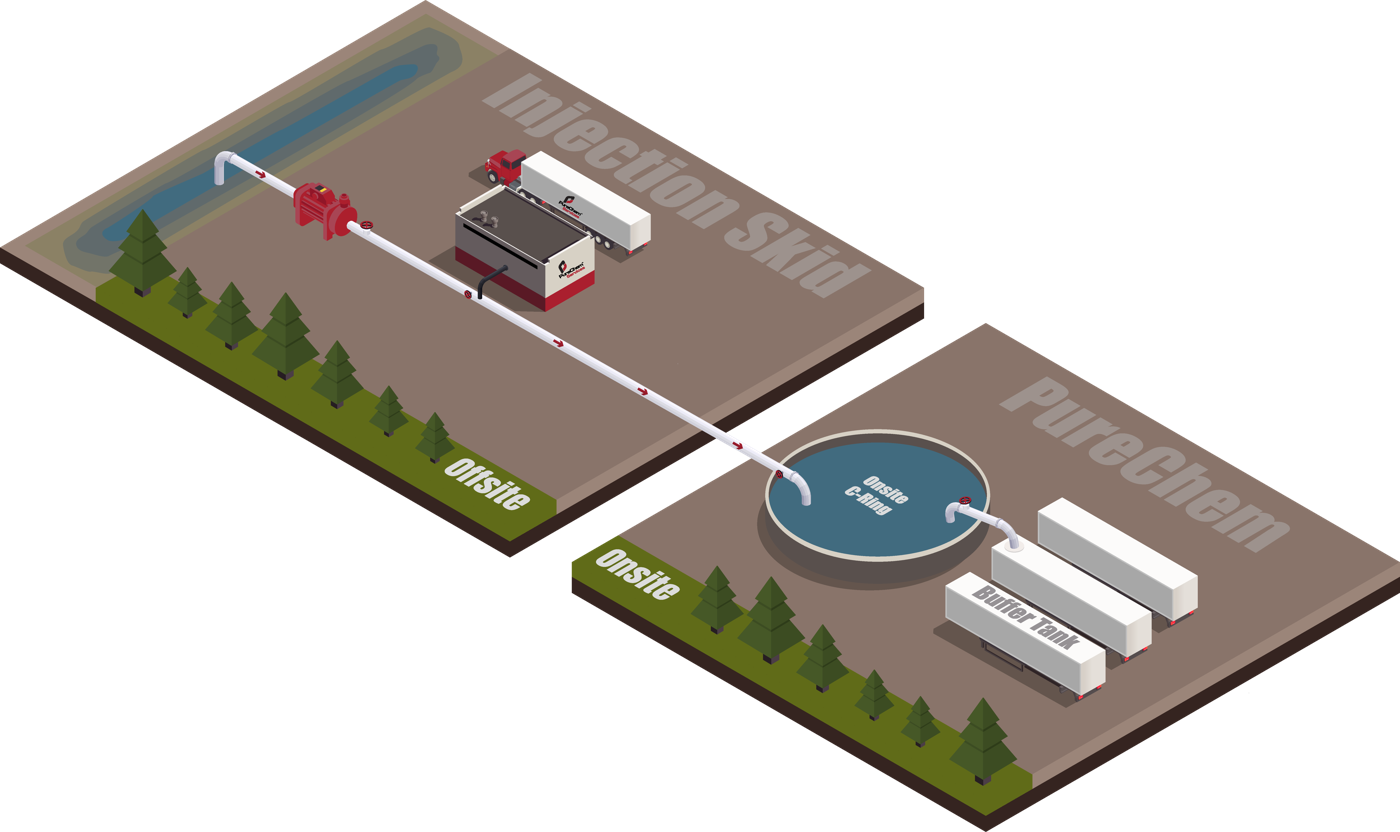
Our injection skids provide the precision required to execute water treatment and transfer on the fly. They are engineered to handle friction reducer injection, mitigate water transfer issues, keep your frac operation moving smoothly, and ensure the needed water volumes arrive on site, reducing NPT.
Maximize your operational potential with a system designed to increase transfer rates by 1.5–2x, as proven in our case studies. High-capacity pumps support flow rates up to 100 L/min per unit, ideal for high-rate slickwater and HVFR operations.
Automated control systems ensure chemical dosing remains within design setpoint, preventing over-treatment and chemical waste.
Designed to address common water transfer bottlenecks, our skids integrate seamlessly into existing water transfer lines to ensure consistent deliverability, with high-pressure capability and integrated storage.